
Dust Control and Explosion Safety in Pressed Candy OEM: Extraction and Housekeeping
The most underestimated risk in a tableting hall is not the press itself but the fine powder suspended in the air. Every stage of pressed candy production, from dispensing and granulation through milling to compression, generates dust, and accumulated dust affects changeover quality and cross-contamination control while also carrying occupational health and explosion consequences. Auditors tend to focus on the tablet press and packing line and rarely ask about extraction or hazardous area classification, yet those two subjects reveal more about a manufacturer's discipline than almost anything else. This article sets out, from the production side, where dust originates in pressed candy OEM, how extraction should be configured, how zones and electrical equipment are selected, and how monitoring and cleaning verification are actually run.
1. Where the dust comes from
Control starts with knowing which steps generate it. Dispensing is the most concentrated source, since tipping powder from a bag into a hopper releases a large plume. Milling and screening after granulation follows, as granules tumble and abrade against the mesh and generate fines. The press itself emits fines continuously during feeding, scraping and ejection, particularly with deep fill depths or material already high in fines. Supporting operations such as comminution, final blending and reworking rejected tablets contribute further. Generation rate depends heavily on material properties: a high fines fraction, low bulk density and poor flow all make dust worse. For that reason a plant measures generation intensity step by step before specifying extraction rather than installing identical air volumes everywhere.
2. Configuring extraction with intent
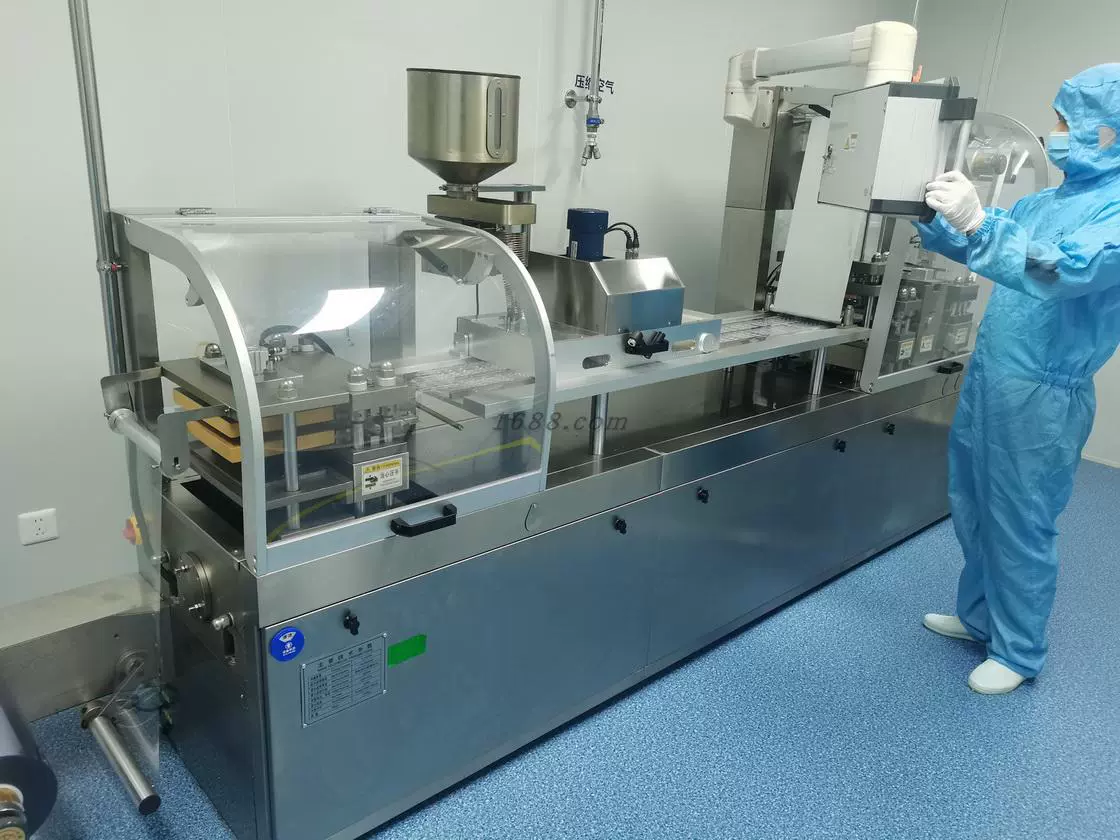
Maximum air volume is not the answer; the configuration has to follow a logic. The usual approach combines local capture with central collection, placing enclosed or semi-enclosed hoods at the source so that a modest airflow captures dust before it disperses, which is far more effective than general extraction at ceiling level. Ducting needs sufficient velocity to keep particles entrained without excessive bends that add resistance. On equipment selection, bag houses suit high volumes and coarser particles, while cartridge collectors occupy less floor space and filter finer, suiting constrained rooms. Hygroscopic dust requires insulated housings and appropriate cleaning to stop the media blinding. Pulse jet cleaning suits continuous operation better than mechanical shaking because differential pressure stays stable between production runs.
3. Hazardous area zoning and electrical selection
Most food powders are combustible, and once concentration reaches the lower explosion limit an ignition source is all that is missing. Plants classify dust explosion hazardous areas accordingly: interiors of collectors and silos as zone 20, the surroundings of dust-generating equipment as zone 21 or 22 depending on release frequency. Each zone carries different equipment requirements, with zone 20 needing intrinsically safe or encapsulated devices and zones 21 and 22 allowing dust-protected enclosures with limited surface temperature. Equally important are equipotential bonding and earthing to prevent electrostatic discharge, antistatic filter media and conductive ducting, and explosion isolation or venting between the collector and the room so a deflagration cannot propagate along the duct. These provisions cost little at design stage and a great deal to retrofit.
4. Monitoring concentration and protecting operators
Management means turning invisible dust into numbers. Plants should periodically measure total and respirable dust at the dispensing, milling, compression and dust discharge positions, and compare results against occupational exposure limits, adding engineering controls or changing work method wherever limits are exceeded. Personal protective equipment is the last line: high-risk dispensing roles need certified respirators and fit checks. Sedimentation is worth tracking too, using settle plates observed on a schedule, since a rising deposition rate signals falling extraction performance or incomplete cleaning. These records also serve as credible evidence during a customer audit, and carry more weight than any assurance given verbally during a walkthrough.
5. Changeover and cross-contamination control
Dust control and changeover quality are two faces of the same problem. Dust collecting in equipment crevices, duct interiors and ceiling voids is the principal route for cross-contamination on shared lines. Effective cleaning goes beyond wiping visible surfaces: it means stripping removable parts, addressing dead legs, and handling ductwork and collection bins separately. Verification usually combines visual inspection with swab sampling, while higher-risk products may be checked for a residual marker or by a general indicator such as total organic carbon. Scheduling matters as well, with active or allergen-containing products run last and followed by full cleaning. Where one collector serves several lines, the filter media itself may need changing or cleaning between products, otherwise the extraction system becomes the contamination pathway.
6. What brand owners should ask during an audit
A few specific questions reveal dust management maturity quickly. First, whether collector airflow and filter area were matched to measured generation, and whether velocity and differential pressure have been tested. Second, whether hazardous areas have been classified and whether equipment in those zones carries certification and maintenance records. Third, whether local capture exists at dispensing and whether operators are properly protected. Fourth, ask for the most recent workplace dust concentration report. Fifth, inspect the dust collection bins and the collector room, because that location reflects daily discipline more honestly than any presentation. None of these questions require specialist knowledge, and the answers usually tell you more than brochures do. A plant that manages dust well is rarely weak elsewhere.
Related Products
Glycerol diester coffee OEM OEM OEM OEM OEM meal replacement coffee MCT live broadcast same solid beverage source manufacturer | GLP-1 Semaglutide Satiety & Fat Blocker Tablets | Custom Pressed Candy OEM Manufacturing
About Guangzhou Mesen Health Biotechnology Co., Ltd
Guangzhou Mesen Health Biotechnology Co., Ltd is located in the Huashan Science and Technology Park, Huadu District, Guangzhou. The company has focused on OEM and ODM services for the big health industry for nearly 20 years, operating dedicated research, production, sales and management centres, and maintaining long-term strategic partnerships with well-known Chinese medicine colleges and research institutions. Capabilities span pressed candy, gummies, capsules, solid beverages, herbal teas, plant beverages, protein powders, dietary supplements and enzyme jelly - from formulation development through contract manufacturing. For details on minimum order quantities, sampling lead times and quotations, see our manufacturing advantages and product range, or contact us for a tailored proposal.
Further Reading




