
Pesticide Residue Control in Herbal Tea OEM: Traceability, Testing and Suppliers
The defining difference between herbal tea and a synthetic tablet is that the raw material grows in a field. Flowers, fruits, leaves and roots pass through cultivation and harvest where pesticides, atmospheric deposition and soil uptake can all leave residues, and no downstream process genuinely removes them. Once a finished batch fails a residue limit, the loss is not one batch but potentially the brand's market access. This article explains, from the manufacturing side, where residue and heavy metal risk originates in herbal tea OEM, how origin traceability actually works, how a test panel should be designed and read, and how supplier qualification and change control are put into practice. We treat raw material control as the first gate in the process.

1. Where residue risk comes from
Risk arrives at roughly three levels. The first is direct use during cultivation, including insecticides, fungicides and herbicides, where an insufficient pre-harvest interval carries residues into the material. The second is environmental transfer, since drift from neighbouring fields, irrigation water and historical soil contamination are all taken up by the plant, and growers cannot fully control these. The third is post-harvest handling, covering fumigants applied against insects and mould plus cross-contamination in storage and transport. Heavy metals belong alongside these, originating mainly from soil background and industrial pollution, with root and rhizome materials typically concentrating more. The implication is simple: asking a supplier for one test report is nowhere near enough, and control has to extend into cultivation and harvest.
2. Making origin traceability real
Traceability is not a QR code; it needs a documented chain behind it. A working system includes a defined growing area, preferably fixed production zones or contracted bases rather than sourcing that moves each season; cultivation records covering variety, planting date, inputs applied and harvest date; grower logbooks that the manufacturer audits periodically; and a unique lot number per delivery that traces upward to the plot and downward to the finished batches using it. Smaller manufacturers often manage lot-level tracing only, not plot-level, which forces an unnecessarily wide recall when something goes wrong. Brands evaluating a plant can ask one question that separates depth from decoration: for a given finished batch, which plot did the material come from?
3. Designing the test panel
Testing verifies, but panel design determines whether it means anything. At the baseline, the panel should follow the applicable product standard and national food safety limits, covering commonly encountered high-risk pesticides and heavy metals. Beyond that, it should reflect the material: fumigant residues for flowers, heavy metals for roots, and destination-market prohibited substances for imported botanicals. Frequency needs to be realistic, since full panel testing on every lot is unaffordable; a sensible pattern runs routine items per lot with periodic full scans scheduled by supplier risk, retaining samples for retest. Judgement must account for differing limits between markets, with export requirements often stricter than domestic, so the strictest applicable limit should drive design. Reports should always be read with the laboratory's accreditation and method detection limit in mind, because an unsuitable method produces a meaningless result.
4. Supplier qualification and tiered control
Material safety ultimately rests with the supplier, so qualification must be rigorous. Approval should cover licences and certifications, growing environment, cultivation and harvest practice, processing capability, testing capability and historical performance, with on-site audit where warranted. Approval is not permanent: suppliers should be tiered by delivered quality, with higher-risk ones facing increased testing frequency and sampling rates while consistently strong ones earn reduced routine testing but retain periodic full scans. Change control is the most neglected part, because a change of growing area, processing method or even packaging material can introduce new risk, and suppliers should be contractually required to notify in advance for reassessment. The quality agreement should allocate responsibility for exceedances, recall cooperation and indemnity, clauses that look excessive beforehand and become the only workable basis afterwards.

5. What processing can and cannot do
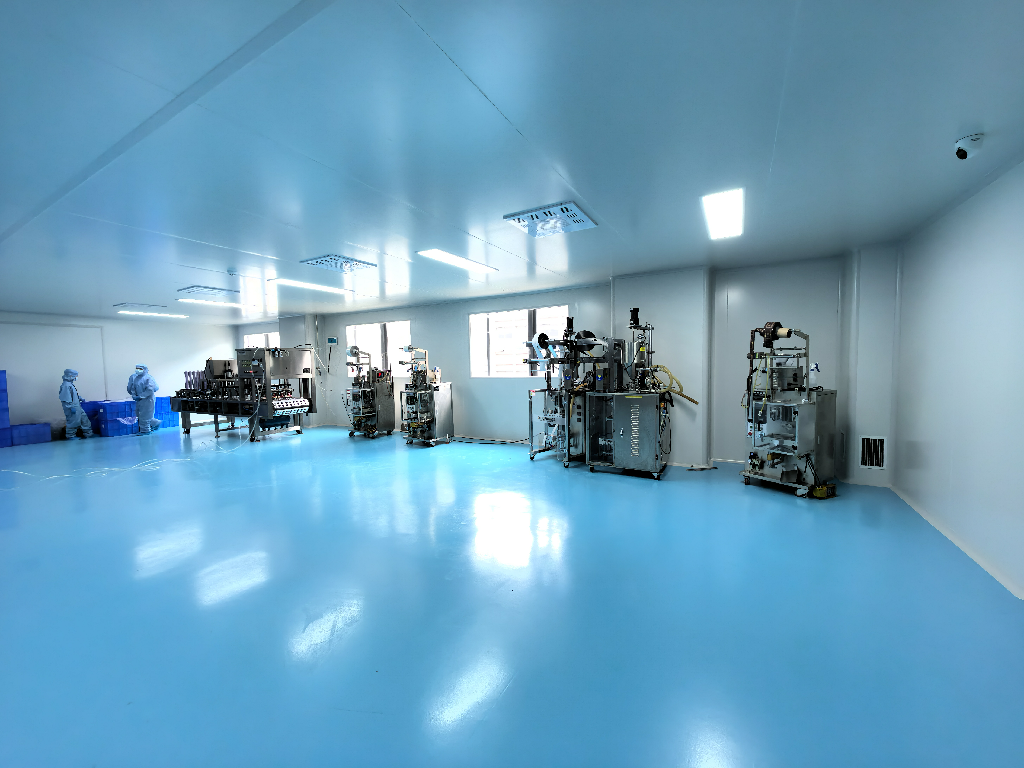
Processing cannot remove residues, but sound practice prevents additional problems and avoids adding new ones. Washing removes some surface contamination and soil, and helps with leaf, flower and fruit materials, though water quality and contact time need control to avoid leaching water-soluble actives. Sorting and destoning removes mouldy, insect-damaged and foreign material, which matters for microbiological and sensory results. Drying requires controlled temperature and time to reach the moisture target without damaging active constituents. Metal detection and foreign body rejection should be standard stations as the final barrier against physical hazards. Warehousing needs zoned stacking, clear labelling, controlled temperature and humidity, and pest control that avoids chemical treatments causing secondary contamination. The value of processing here is not introducing further risk.
6. Practical guidance for brand owners
A few measures reduce risk on herbal tea projects. First, ask about growing areas and supplier documentation at quotation stage, because a manufacturer able to produce cultivation records and tiering evidence is usually the safer choice. Second, resist driving material cost to the floor, since price gaps for the same botanical reflect origin, grade and residue management, and the lowest price generally means control at source was sacrificed. Third, state the destination market's limits at project start, particularly for export, rather than adding requirements after commercial production. Fourth, require retained samples so any anomaly can be retested and traced. Fifth, write report frequency and format into the contract, turning verbal assurances into enforceable terms. These steps add discussion time at the front end and cost far less than a single recall.
Related Products
Grape Oolong Fruit Tea Blend | Pyramid Tea Bags Herbal Wellness Tea Custom OEM | Corn Silk Herbal Tea | Wellness Herbal Tea Private Label OEM Manufacturer
About Guangzhou Mesen Health Biotechnology Co., Ltd
Guangzhou Mesen Health Biotechnology Co., Ltd is located in the Huashan Science and Technology Park, Huadu District, Guangzhou. The company has focused on OEM and ODM services for the big health industry for nearly 20 years, operating dedicated research, production, sales and management centres, and maintaining long-term strategic partnerships with well-known Chinese medicine colleges and research institutions. Capabilities span pressed candy, gummies, capsules, solid beverages, herbal teas, plant beverages, protein powders, dietary supplements and enzyme jelly - from formulation development through contract manufacturing. For details on minimum order quantities, sampling lead times and quotations, see our manufacturing advantages and product range, or contact us for a tailored proposal.
Further Reading




