
Enzyme Jelly OEM Equipment: Depositing, Sterilisation and Sealing Parameters That Matter
The equipment for enzyme jelly looks simple - cook, deposit, sterilise, seal, four steps. Consistent quality, though, comes from fixing every parameter as a number. In enzyme jelly OEM, a few degrees of difference at depositing or a few minutes in the sterilisation cycle show up in texture, syneresis and microbial results. This guide sets the key parameters in process order.

1. Gel preparation and cooking: where the network starts
Cooking temperature and time decide whether the gelling agent swells fully. Gelatin usually swells in water at 60 to 70 degrees before dissolving at 75 to 85; too high or held too long and gel strength drops. Pectin needs cooking with sugar under acidic conditions to a specific temperature before it will set. The critical controls are filtration after dissolving, to remove unswollen particles and debris, and resting for de-aeration. The most common shortcut here is raising the temperature to save time, which produces a weak gel that weeps later.
2. Depositing: temperature, speed and drop height
Temperature control at depositing tests experience more than anywhere else. Too hot and the mass is thin, entrains air and can deform the mould; too cool and viscosity rises, so dosing drifts and surfaces finish uneven. Gelatin systems normally run at 75 to 85 degrees, pectin slightly higher. Control the drop height between nozzle and mould, keeping it as short as practical, and the depositing speed, to avoid turbulent air pickup. Formulas with puree or juice carry higher risk and need a vacuum de-aeration stage before depositing.
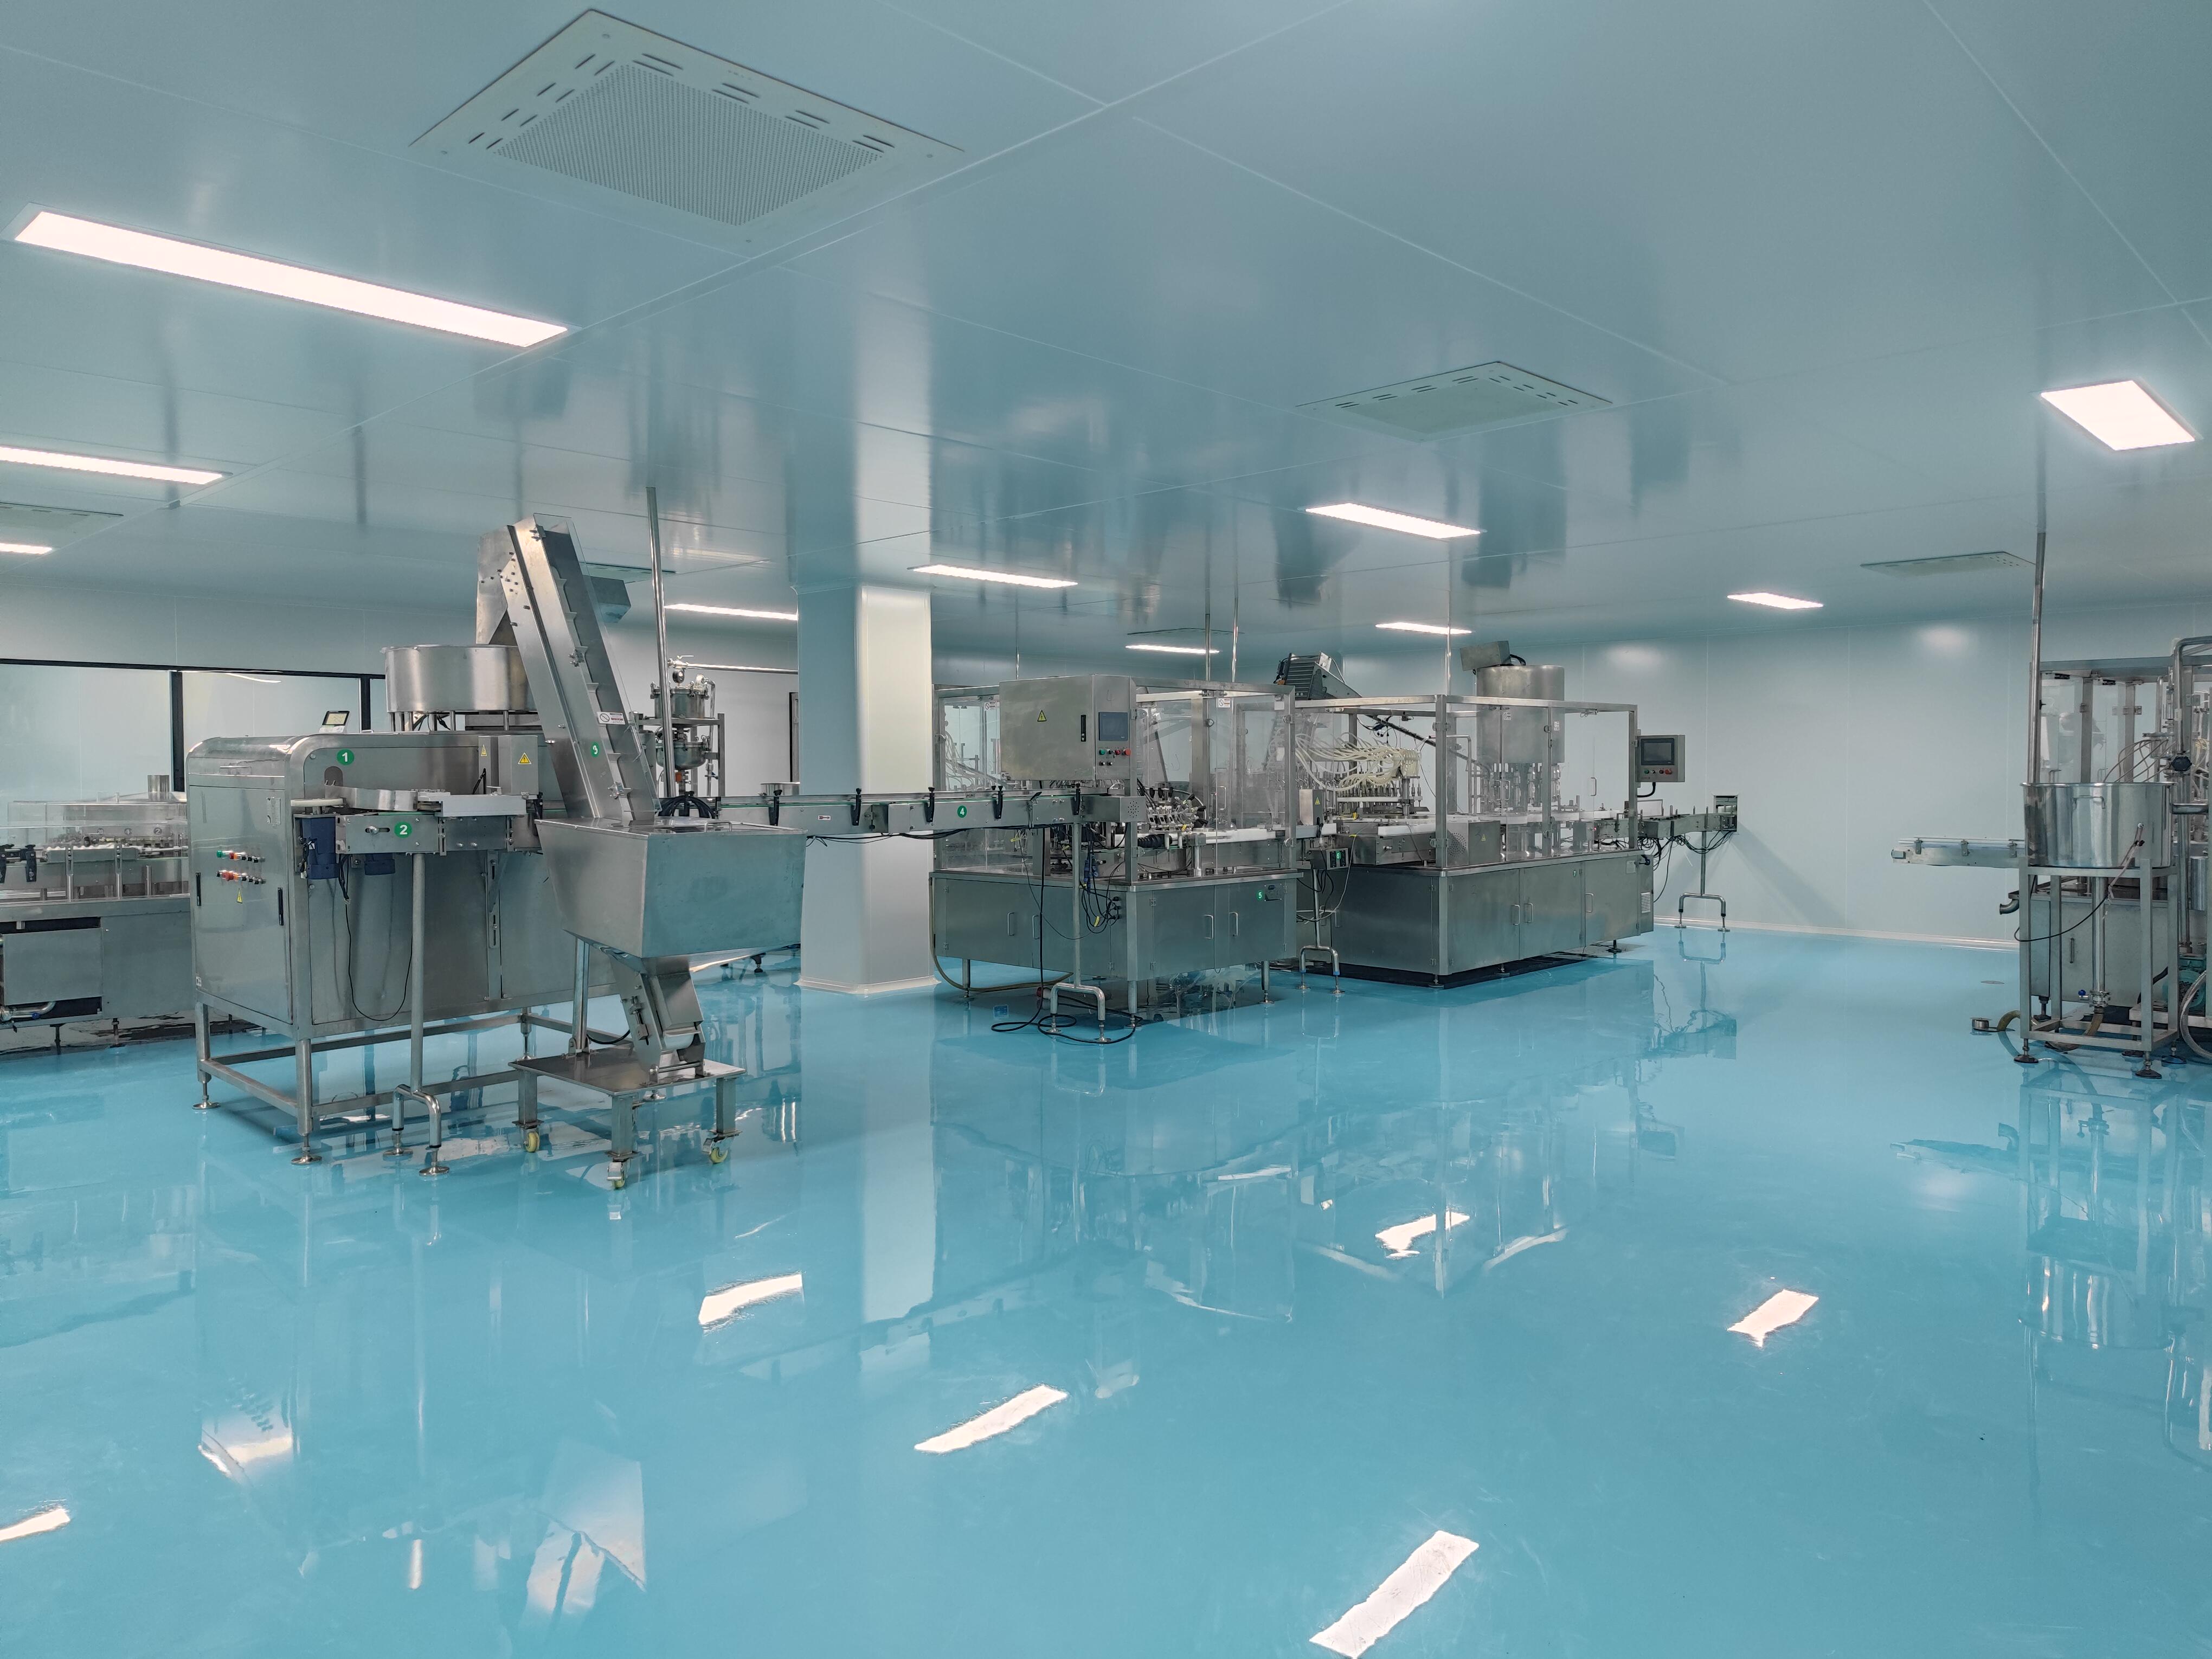
3. Drying: the triangle of temperature, humidity and time
Drying-room settings determine finished moisture and water activity, and through them texture and microbial stability. Typical values are 25 to 30 degrees, 30 to 40 percent relative humidity and 18 to 36 hours, depending on piece size and gelling system. Too warm and a skin forms that traps internal moisture; too humid and drying crawls while mould risk climbs. Disciplined plants record the drying curve for every batch and sample moisture and water activity before release to the next step, rather than judging by touch. Airflow uniformity matters as much as the set point: a room with dead corners turns out trays that differ by several points of moisture within the same batch.
4. Sterilisation: pasteurisation or retort
Sterilisation has to clear microbiology without destroying the gel network. Two routes dominate. Pasteurisation, 85 to 90 degrees held for 15 to 30 minutes, has little effect on texture and suits acidic formulas at pH 4.5 or below. High-temperature treatment, 105 to 121 degrees for a short time, suits neutral or low-acid products but tends to soften the gel and drive syneresis. The choice follows pH and water activity: products that are acidic and low in water activity inhibit microbes on their own and only need pasteurisation.
5. Sealing: the last gate on shelf life
Seal quality on stick packs and cups decides shelf life directly. Heat sealing has three variables - temperature, pressure and dwell - and each must be validated for the material in use, whether aluminium laminate film or a PP cup with foil lid. Under-set parameters produce a weak seal that looks fine but leaks slowly; over-set ones shrink the material at the seam and wrinkle it. Plants should confirm parameters on every sealing machine and run seal integrity sampling by vacuum decay or dye ingress. Then check the seal area for product contamination, since sugar residue is the leading cause of weak seals. File the inspection results with the batch record rather than with the machine, or there is nothing to review when a complaint arrives.

6. Turning parameters into process documents
A mature contract manufacturer writes all of the above into process specifications: temperature, time, speed and humidity range for each step, plus the action to take when a value drifts. The benefit is that shift changes and staff turnover no longer affect consistency, and a brand has something concrete to review during an audit. When visiting a plant, ask to see the process specification for one product and the production records for the last three batches - whether those documents exist is one of the most reliable reads on how maturely the plant is managed.
Related Products
Extra Strength Orange Enzyme Jelly with Prebiotics | Fruit-Flavored Cup Jelly Private Label OEM Manufacturer | Collagen Fruit & Vegetable Enzyme Jelly with Prebiotics | Custom Extra Strength Jelly OEM Factory
About Guangzhou Mesen Health Biotechnology Co., Ltd
Guangzhou Mesen Health Biotechnology Co., Ltd is located in the Huashan Science and Technology Park, Huadu District, Guangzhou. The company has focused on OEM and ODM services for the big health industry for nearly 20 years, operating dedicated research, production, sales and management centres, and maintaining long-term strategic partnerships with well-known Chinese medicine colleges and research institutions. Capabilities span pressed candy, gummies, capsules, solid beverages, herbal teas, plant beverages, protein powders, dietary supplements and enzyme jelly - from formulation development through contract manufacturing. For details on minimum order quantities, sampling lead times and quotations, see our manufacturing advantages and product range, or contact us for a tailored proposal.
Further Reading


